High-purity bioactive botanical powders, cold-pressed oils, and micro-encapsulated formulations engineered to meet international pharmacopeia standards.





An authoritative analysis on global botanical processing shift from traditional crude extracts to high-potency, standardized functional actives.
The global botanical extracts market is undergoing a paradigm shift driven by consumer demand for transparent, clean-label, and sustainably sourced ingredients. Modern formulators across pharmaceuticals, functional foods, and cosmeceuticals are abandoning synthetic active molecules in favor of bio-identical botanical compounds verified by rigorous chromatographic fingerprinting.
Standard crude plant powders no longer suffice for advanced nutraceutical delivery systems. The market demands liposomal encapsulation, micro-emulsification, and water-dispersible formulations designed to overcome poor physiological absorption rates, ensuring active phytochemicals cross cellular barriers effectively.
Global regulatory agencies, including the US FDA, European Food Safety Authority (EFSA), and NMPA, have heightened requirements for active marker quantification (e.g., Withanolides, Ellagic Acid, Polyphenols). Modern functional extract factories must integrate real-time batch standardization and analytical validation.
Bridging traditional botanical wisdom with modern biotechnology to supply premier ingredients across the globe.
Shenzhen Bluidge Biology Co., Ltd. is a professional herbal extract manufacturer and botanical ingredient supplier based in Shenzhen, China. The company specializes in the research, development, production, and global export of high-quality plant-based extracts for cosmetics, food, dietary supplements, and pharmaceutical applications.
With advanced extraction technologies and strict quality control systems, Bluidge Biology produces a wide range of natural herbal extracts, including water-soluble, oil-soluble, and standardized active ingredients. These botanical materials are widely used in skincare formulations, functional foods, health supplements, and personal care products.
The company integrates modern biotechnology with traditional botanical knowledge to ensure high purity, stability, and bioactivity in every extract. Each product undergoes rigorous testing to meet international quality and safety standards, ensuring consistency and reliability for global customers.
Shenzhen Bluidge Biology Co., Ltd. provides OEM and customized solutions, supporting clients with formulation development, ingredient selection, and bulk supply services. The company is committed to innovation in natural ingredients and sustainable sourcing practices, meeting the growing global demand for clean-label and plant-based solutions.
By combining scientific research, advanced production capabilities, and international service experience, Bluidge Biology has become a trusted partner in the herbal extract industry, delivering high-performance botanical ingredients to customers worldwide.
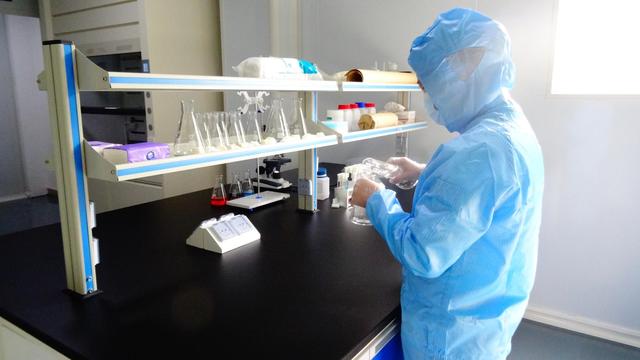
Our analytical labs employ High-Performance Liquid Chromatography (HPLC), Gas Chromatography-Mass Spectrometry (GC-MS), and Atomic Absorption Spectroscopy (AAS) to verify pesticide zero-residue levels, heavy metal limits, and exact bioactive concentration markers.
Deploying green engineering and quantum-yield extraction methodologies to maximize molecular integrity.
Liposomal technologies shield active molecules (such as Boswellia extracts and hydrophobic polyphenols) within phospholipid bilayers. This improves digestive protection, enhances cell membrane penetration, and provides sustained release profiles in liquid and capsule dosage formats.
By utilizing carbon dioxide at supercritical temperatures and pressures, lipophilic phytochemicals (such as Turmeric Essential Oils) are extracted without thermal degradation or organic solvent residues, preserving native terpene and sesquiterpene profiles.
Targeted enzymatic digestion breaks down complex plant cell walls, releasing bound polyphenols and polysaccharides. Molecular weight filtration via ceramic ultrafiltration membranes ensures precise molecular cutoffs for high-purity concentrates.
| Extraction Technology | Target Bioactive Class | Solvent System | Purity Threshold | Key Advantage |
|---|---|---|---|---|
| Liposomal Nano-Carrier | Boswellic Acids, Lipophilic Phenols | Aqueous Phospholipid Matrix | Standardized 40%-65% | 350% Higher Bio-availability |
| Supercritical SFE-CO2 | Essential Oils, Curcuminoids, Terpenes | Supercritical Fluid (CO2) | Up to 98% Volatiles | 100% Solvent Free & Solvent Pure |
| Ultrasonic-Assisted Hydro-Alcoholic | Withanolides, Adaptogenic Glycosides | Ethanol/Water Eco-System | Standardized 2.5%-10% | Low-Thermal Structural Preservation |
| Spray Drying Micro-Encapsulation | Polysaccharides, Algae Phycocyanin | Purified Deionized Water | Instant Water Soluble | Enhanced Thermal & Thermal Stability |
Engineered ingredients tailored for specific end-product delivery mechanisms across global health sectors.
High-purity botanical extracts engineered for anti-aging, UV damage protection, DNA cellular repair, and inflammatory pathway down-regulation. Solutions feature clear solubility for serums and stable oil-emulsions for creams.
Water-dispersible powders and drops offering thermal stability during pasteurization. Designed for instant drink premixes, functional stick-packs, and functional bakery lines without compromising taste or sensory clarity.
Standardized adaptogenic extracts and dense superfood powders customized for hard capsules, softgels, tableting, and fast-acting liquid drops aimed at stress resilience, longevity, and metabolic support.
Ultra-pure active pharmaceutical ingredients (APIs) extracted under strict cGMP protocols, providing documented HPLC assay values, ultra-low heavy metals, and consistent batch-to-batch chemical profiles.
Meeting the strict regulatory architectures of North America, Europe, Asia-Pacific, and Middle Eastern markets.
Our extraction lines operate under ISO 9001, ISO 22000, HACCP, Halal, and Kosher regulatory certifications. Full documentation dossiers including Certificate of Analysis (COA), Safety Data Sheets (SDS), Technical Data Sheets (TDS), and Allergen Statements accompany every bulk shipment.
By establishing localized warehousing strategies and maintaining strategic alliances with premier global freight networks, Bluidge Biology ensures rapid customs clearance, seamless DDP/FOB terms, and temperature-controlled logistics to prevent bioactive degradation during transport.
From 1kg aluminum foil vacuum pouches for high-potency research ingredients to 25kg fiber drums for industrial manufacturing, alongside turnkey end-consumer retail drop bottles (30ml/60ml), we provide fully customizable private-label packaging.
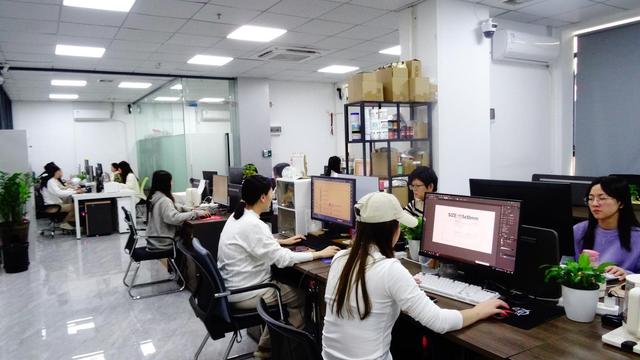
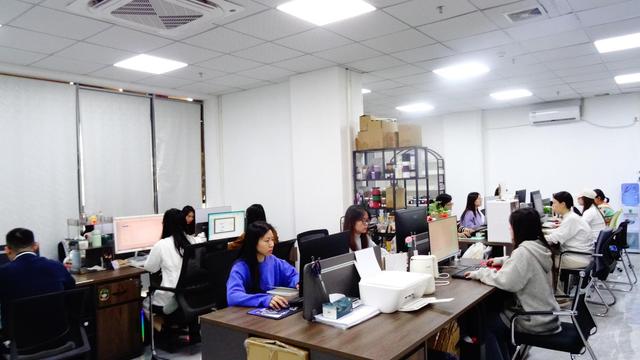
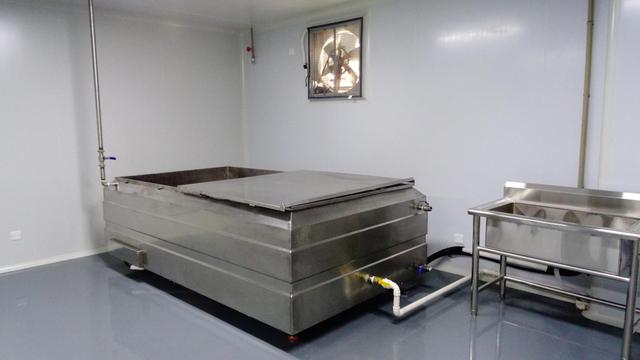
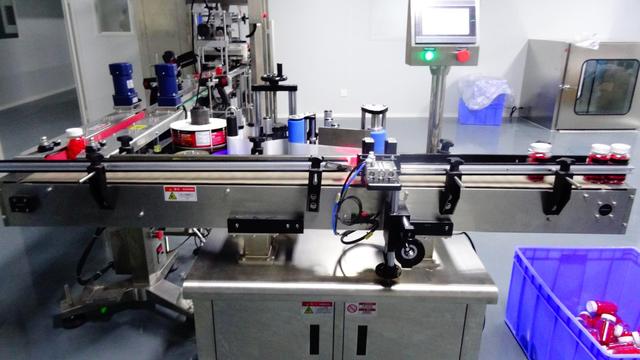
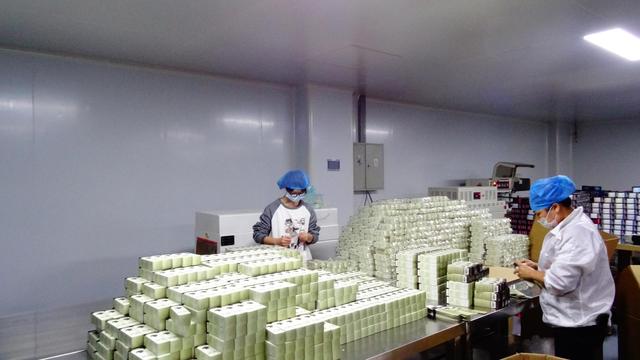
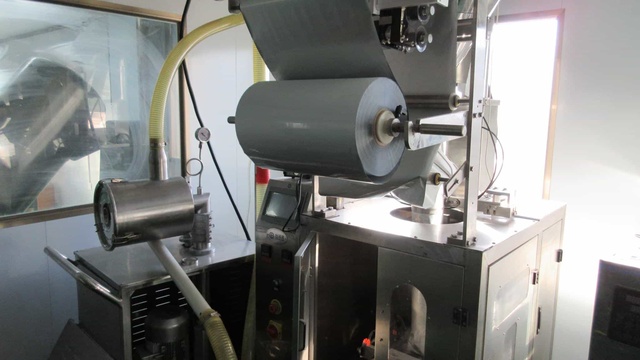
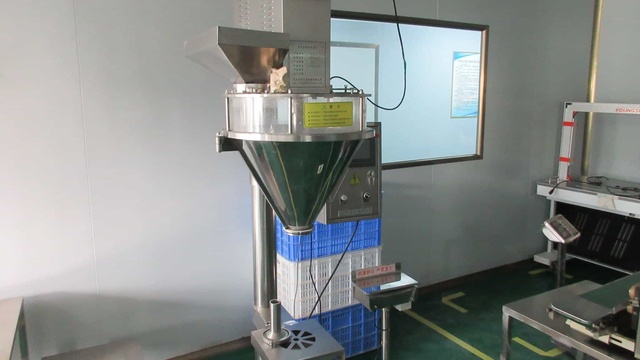
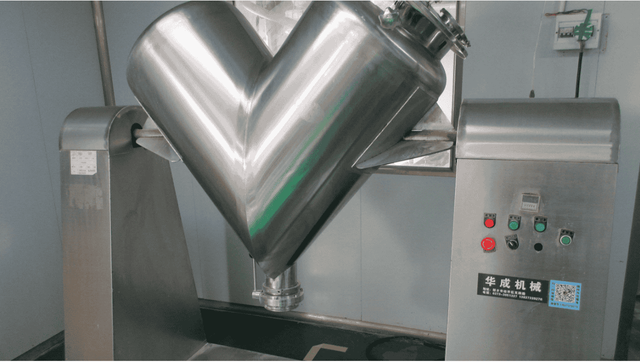
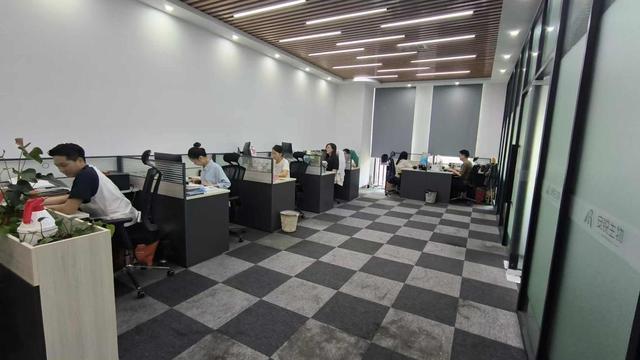
Inside Shenzhen Bluidge Biology Co., Ltd. - State-of-the-art facilities engineered for safety, purity, and scientific precision.
Detailed answers regarding standardization metrics, custom encapsulation technologies, and international supply logistics.
Micro-algae extracts, cosmetic grade polyphenols, and liposomal compounds for advanced wellness product lines.


 Bluidge Biology