Advanced standard biological derivatives featuring supreme purity, stability, and customized molecule weight profiles.




Industry Whitepaper Insight: Navigating Global Herbal Ingredients Trends
The global life science, clean-label cosmetic, and functional food sectors are moving past raw botanical powders. Standardized extraction with validated pharmaceutical-level molecular marker analysis defines the modern landscape.
As international consumer regulatory frameworks restrict synthetic additives, companies are rushing to procure complex organic compounds that offer high physiological efficiency. Today’s buyers demand non-GMO, pesticide-free, and solvent-safe raw materials featuring documented active secondary metabolites like flavonoids, polyphenols, oleanolic acids, and saponins.
To sustain market dominance, global brands must select supply chain partners who maintain complete control over raw material cultivation, use advanced green chromatography, and provide third-party validation documents (HPLC, GC-MS) on every shipment batch.
Moving from simple extraction ratios (e.g. 10:1) to absolute concentration testing of targeted compounds (e.g. Forsythin at 98%, Luteolin at 98%, Dimethoxyflavone at 10%).
Green water-soluble extraction methodologies that minimize organic solvent residues to ensure total compatibility with strict FDA and European Food Safety Authority (EFSA) regulations.
Addressing the critical risk parameters identified by procurement specialists in multi-national food, cosmetic, and pharmaceutical corporations.
Total trace-back mechanisms from regional wild harvesting or GAP-certified cultivation bases straight to final packaged containers. Eliminates heavy metal contamination and cross-contamination risks.
Batch-to-batch consistency managed through standardized chemical profiles. Using chromatographic fingerprinting technology, we guarantee the active ingredients remain identical across global production lines.
Complete botanical and chemical safety dossiers including Kosher, Halal, ISO22000, and FDA compliance logs to bypass international trade barriers seamlessly.
Industry-Leading Scientific Extraction and R&D Capabilities
Shenzhen Bluidge Biology Co., Ltd. is a professional herbal extract manufacturer and botanical ingredient supplier based in Shenzhen, China. The company specializes in the research, development, production, and global export of high-quality plant-based extracts for cosmetics, food, dietary supplements, and pharmaceutical applications.
With advanced extraction technologies and strict quality control systems, Bluidge Biology produces a wide range of natural herbal extracts, including water-soluble, oil-soluble, and standardized active ingredients. These botanical materials are widely used in skincare formulations, functional foods, health supplements, and personal care products.
The company integrates modern biotechnology with traditional botanical knowledge to ensure high purity, stability, and bioactivity in every extract. Each product undergoes rigorous testing to meet international quality and safety standards, ensuring consistency and reliability for global customers.
Shenzhen Bluidge Biology Co., Ltd. provides OEM and customized solutions, supporting clients with formulation development, ingredient selection, and bulk supply services. The company is committed to innovation in natural ingredients and sustainable sourcing practices, meeting the growing global demand for clean-label and plant-based solutions.
By combining scientific research, advanced production capabilities, and international service experience, Bluidge Biology has become a trusted partner in the herbal extract industry, delivering high-performance botanical ingredients to customers worldwide.
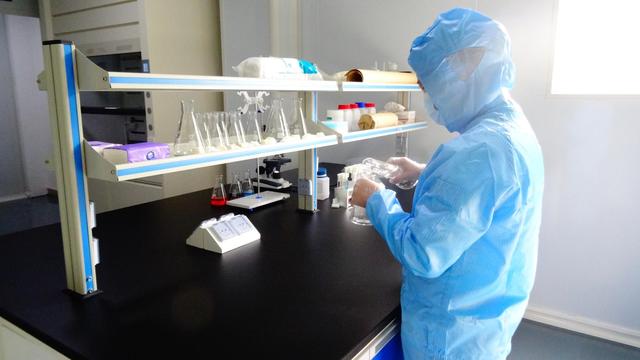
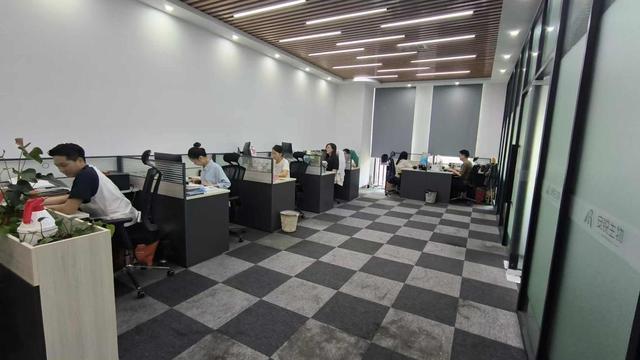
Take an inside look at our state-of-the-art facility: GMP extraction halls, R&D center, clean-rooms, and multi-tier testing laboratories.
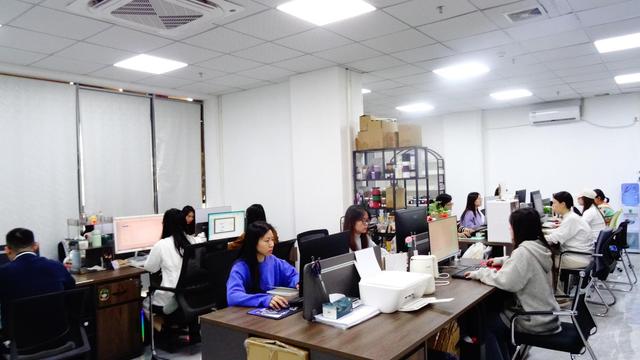
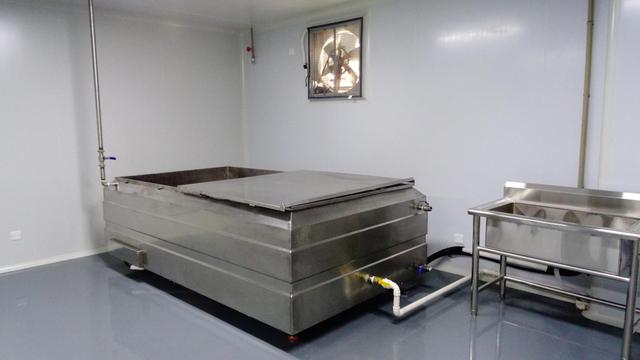
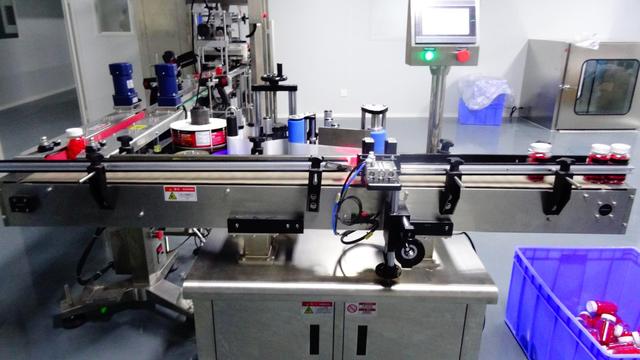
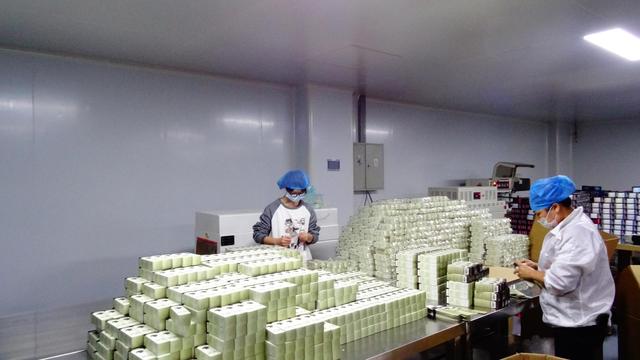
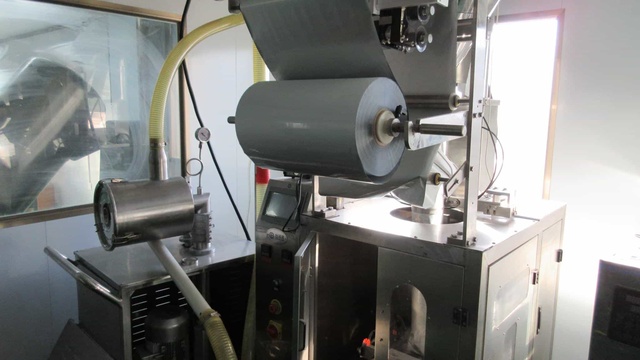
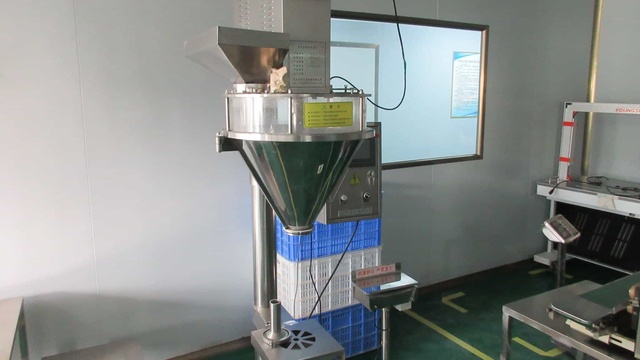
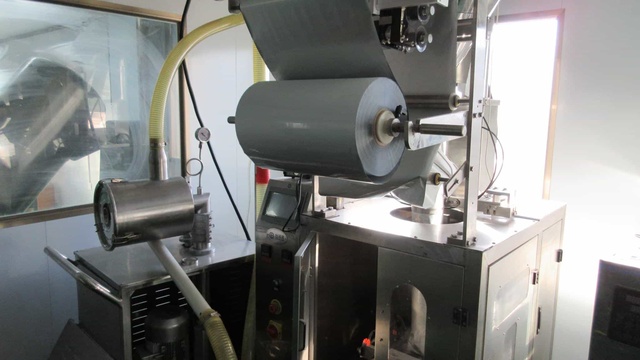
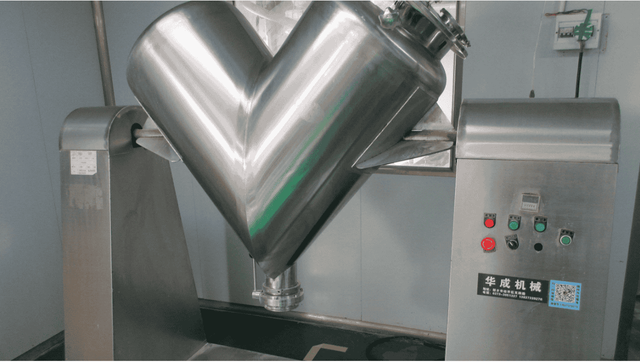
We tailor our plant-derived molecules to meet the specific biochemical needs of four key industry sectors.
Anti-inflammatory and melanin-inhibiting active matrices (like Wild Licorice and Dandelion Root extracts) designed for stable emulsion suspensions.
Immune support and cellular defense extracts (like Reishi Mushroom and Forsythia Fructus powders) optimized for rapid bio-absorption.
Thermally stable natural antioxidants and coloring agents (such as Non-GMO Tomato Lycopene and Pomegranate Fruit powder) designed for long shelf-life dairy and beverages.
High-purity essential oils, oil-soluble arnica complexes, and shampoo-to-gel formulations that perform well in low-pH surfactants.
Our quality verification system monitors every step from seed sourcing to global logistics. We handle all compliance needs to ensure a smooth import process for our clients worldwide.
Reliable Delivery and Customer Care Across Every Region
To serve the European, North American, and Asia-Pacific markets, Shenzhen Bluidge Biology Co., Ltd. provides comprehensive logistics solutions. We coordinate custom clearance protocols and offer direct DDP shipping options to simplify international trade.
Our global support team helps customers address regulatory challenges, review product formulations, and perform active ingredient testing. We maintain stable production schedules and raw material stocks to shield your supply chain from seasonal shortages and price spikes.
Our engineering vision: upgrading extract purity and efficiency through greener chemical processing.
Find answers to common technical, logistics, and quality questions about sourcing botanical ingredients from China.
Complete your sourcing review with our highly active ingredients, botanical drops, and specialized formulations.



 Bluidge Biology