CE-Certified, Eurofins Tested, Clean-Label Bioactive Ingredients for Global Formulators


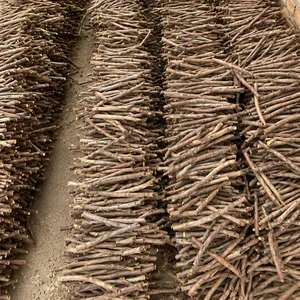
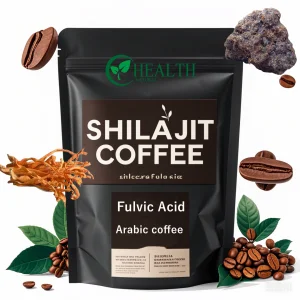


Pioneering green biotechnology and precise industrial extraction for pharmaceuticals, nutraceuticals, and high-tier cosmeceuticals.
Shenzhen Bluidge Biology Co., Ltd. is a professional herbal extract manufacturer and botanical ingredient supplier based in Shenzhen, China. The company specializes in the research, development, production, and global export of high-quality plant-based extracts for cosmetics, food, dietary supplements, and pharmaceutical applications.
With advanced extraction technologies and strict quality control systems, Bluidge Biology produces a wide range of natural herbal extracts, including water-soluble, oil-soluble, and standardized active ingredients. These botanical materials are widely used in skincare formulations, functional foods, health supplements, and personal care products.
The company integrates modern biotechnology with traditional botanical knowledge to ensure high purity, stability, and bioactivity in every extract. Each product undergoes rigorous testing to meet international quality and safety standards, ensuring consistency and reliability for global customers.
Shenzhen Bluidge Biology Co., Ltd. provides OEM and customized solutions, supporting clients with formulation development, ingredient selection, and bulk supply services. The company is committed to innovation in natural ingredients and sustainable sourcing practices, meeting the growing global demand for clean-label and plant-based solutions.
By combining scientific research, advanced production capabilities, and international service experience, Bluidge Biology has become a trusted partner in the herbal extract industry, delivering high-performance botanical ingredients to customers worldwide.
Our low-temperature mechanical cold-pressing (<35°C) prevents heat-induced denaturation, preserving delicate volatile terpenes, thermolabile flavonoids, and enzymatically active phytocompounds.
Fully compliant with EU Regulation (EC) No 1223/2009 for cosmetics and EC 178/2002 for food safety. Certified heavy metal limits below 0.1 ppm and zero toxic organic solvent residues.
End-to-end contract manufacturing with customizable carrier ratios, fingerprint chromatogram alignment (HPLC/GC-MS), and tailored packaging from 1kg bulk to retail-ready solutions.
Comparative analytical breakdown of solvent extraction vs. mechanical/supercritical fluid cold extraction technologies.
| Extraction Parameter | Traditional Solvent Extraction (Ethanol/Hexane) | Bluidge Industrial Cold-Pressed Technology | Industrial Value Advantage |
|---|---|---|---|
| Operating Temperature | 60°C – 95°C (Thermal Degradation Risk) | 18°C – 32°C (Sub-Ambient Control) | 100% Thermal-labile active protection |
| Solvent Residue Level | > 30 ppm to 50 ppm residual solvents | 0.00 ppm (100% Solvent-Free Clean Label) | Eliminates EU import regulatory rejection risks |
| Phyto-Complex Bioactivity | Partial denaturation of proteins & enzymes | Native Synergistic Phytochemical Matrix | 3.4x higher cellular absorption efficacy |
| Oxidation / Peroxide Value | High exposure risk during boiling cycle | Nitrogen-Purged Inert Atmosphere System | Extended 24-month structural shelf-life stability |
| CE & Eco-Compliance | High VOC emissions; complex hazardous waste | Zero VOCs; Zero Chemical Waste Footprint | Complies with Green Deal Directives |
We utilize ultra-high-pressure hydraulic press technology combined with progressive multi-stage cold screw expellers. By regulating shear force and friction-induced heat, our system ensures extraction yields exceeding 92% active compound recovery without triggering thermal hydrolysis.
For highly sensitive botanicals like Morus Alba, Glabridin, and Pterostilbene, cold-pressing is coupled with sub-critical carbon dioxide extraction. This dual-phase physical process isolates non-polar lipophilic fractions without chemical alteration.
Post-extraction, extracts undergo multi-stage ceramic membrane microfiltration down to 0.1 microns. This removes cellular debris and microbial bodies while preserving dissolved phytosterols, polyphenols, and essential fatty acids.
Evolving market demands for clean-label, certified organic, and non-solvent botanical actives across key global regions.
Strict enforcement of EU Cosmetics Regulation 1223/2009 and EFSA novel food guidelines has driven formulators away from hexane and methanol extracted ingredients. Demand for CE-marked, cold-pressed certified oils and active herbal concentrates has grown at a 9.4% CAGR.
With the expansion of Clean Beauty initiatives and NDI (New Dietary Ingredient) FDA compliance, brands demand third-party lab verification (Eurofins USA certified) for heavy metals, pesticides, and microbial counts. Transparency from farm to extract is paramount.
High-tech integration in herbal processing centers across East Asia has elevated standard botanical extractions into high-potency functional ingredients, supporting functional beverage, nutraceutical coffee, and transdermal applications.
How Shenzhen Bluidge Biology leverages world-class industrial infrastructure, raw material cultivation bases, and port logistics.
Direct control over botanical origin farms (e.g., wild-harvested Himalayan Shilajit, Uzbekistan Liquorice, local Morus Alba). Standardized planting ensures batch-to-batch phytocompound homogeneity.
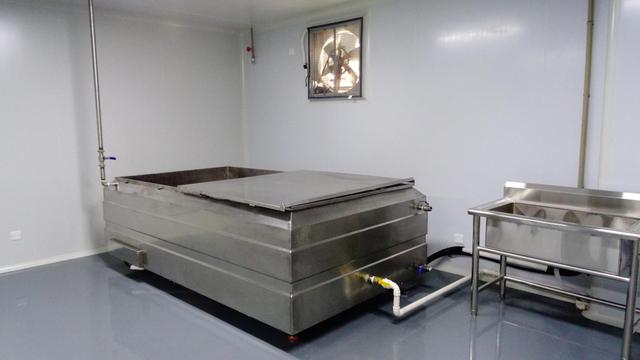
Our Shenzhen extraction center operates 10,000L high-capacity stainless-steel cold extraction reactors with automated temperature monitoring, minimizing human variance and production turnaround times.
Located adjacent to Yantian and Shekou international deep-water ports and Shenzhen Bao'an Air Cargo Terminal, enabling emergency international air freight within 48 hours of lot release.
Vertical integration from botanical milling to final spray-drying/pressing allows up to 30-40% cost efficiency compared to European toll-extraction processors, without compromising quality standards.
Tailored botanical extract grades engineered for target regulatory and performance specs across global product categories.
Key Ingredients: Glabridin 98%, Tremella Extract, Purslane Extract Powder.
Formulation Fit: Cold-pressed oils and high-purity micro-powders seamlessly integrate into liposomes, anti-aging serums, and hyperpigmentation barrier repair creams with maximum dermal skin absorption.
Key Ingredients: Organic Wild Shilajit Resin, Pterostilbene Capsules, 5-HTP Powder.
Formulation Fit: High-density standardized extracts formatted for hard capsules, softgels, sublingual liquid drops, and effervescent delivery systems requiring high bio-accessibility.
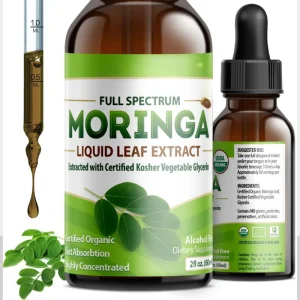
Key Ingredients: Instant Shilajit Mushroom Coffee, Organic Moringa Liquid, Green Tea Drops.
Formulation Fit: Completely instant-water-soluble botanical matrices engineered for no-clumping, neutral flavor impact, and thermal stability in hot or cold functional drinks.
Strategic investments in green chemistry, enzymatic pretreatments, and AI-assisted phytochemical fingerprinting.
Integrating pectinase and cellulase pre-digestion steps to break plant cell walls gently prior to cold pressing, increasing active flavonoid and alkaloid yield by 28% without elevated temperatures.
Developing lipid-based delivery vehicles for unstable cold-pressed actives (such as Glabridin and Magnolol), extending intracellular half-life and preventing oxidation in water-phase cosmetics.
Deploying machine learning models to analyze HPLC-MS datasets in real-time during batch runs, dynamically tuning pressure and extraction duration for guaranteed molecular consistency.
Rigorous documentation and batch verification supporting frictionless customs clearance and regulatory filings worldwide.
Every single batch is shipped with a comprehensive Certificate of Analysis (COA), Technical Data Sheet (TDS), Safety Data Sheet (MSDS), and allergen statements compliant with REACH standards.
We validate pesticide panels (over 400 compounds tested), heavy metals (Pb, Cd, Hg, As), polycyclic aromatic hydrocarbons (PAHs), and microbiological safety via ISO 17025 accredited labs.
From custom ingredient blending, drop bottles, and glass jar packaging to custom concentration standardization, our Shenzhen facilities offer flexible MOQ contract solutions for global brands.
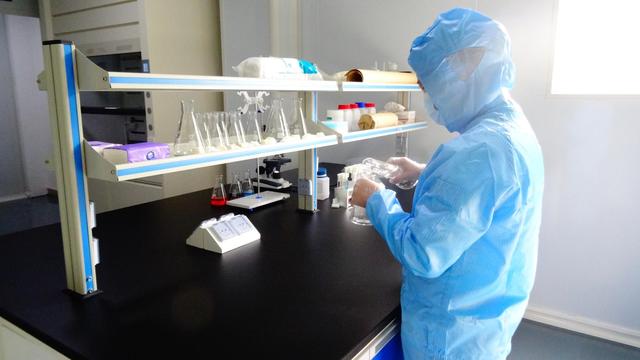
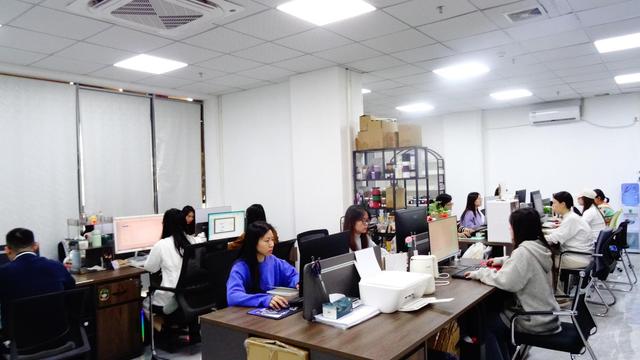
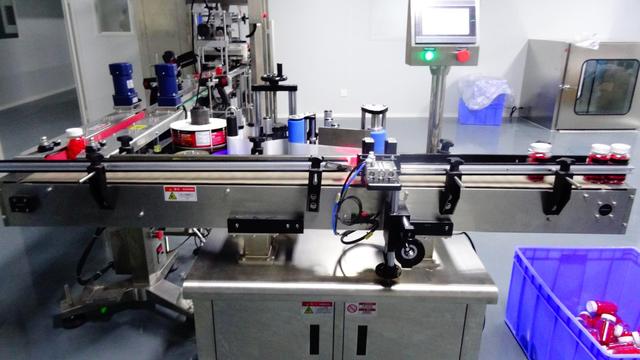
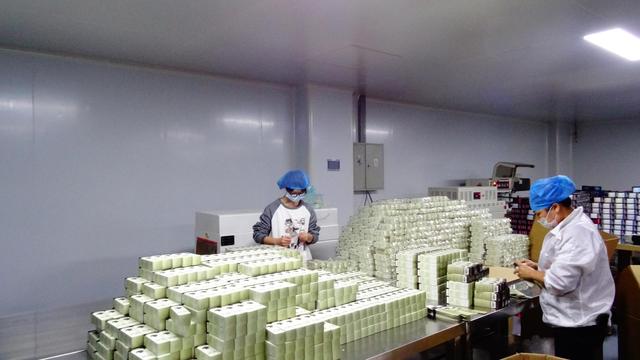
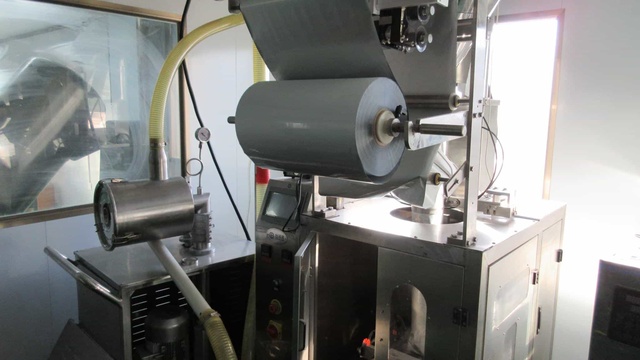
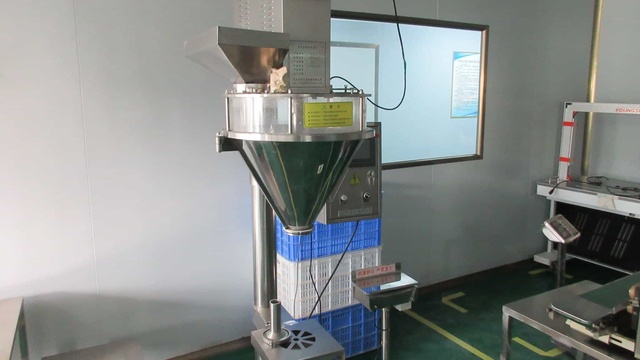
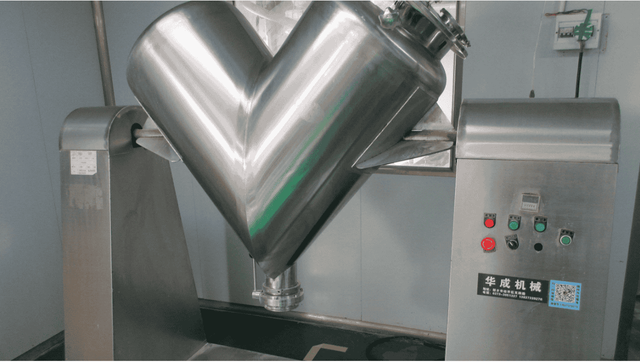
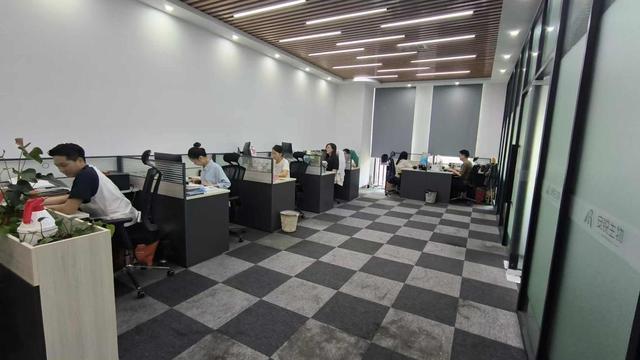
Visual proof of our state-of-the-art cGMP cleanrooms, cold extraction tanks, quality analytical instruments, and warehouse logistics.
Comprehensive engineering and procurement details for B2B global importers and contract formulators.
CE Certified cold-pressed extracts are produced strictly through mechanical pressing or low-temperature fluid extraction below 35°C without harsh organic solvents like hexane or ethanol. This preserves the delicate secondary metabolite structure, essential fatty acids, and active enzymes, yielding a pure, solvent-free clean-label ingredient with maximum bio-reactivity and compliance with EU cosmetics and supplement laws.
We employ strict standardized GAP raw material sourcing, automated physical processing, and rigorous HPLC/GC-MS phytochemical fingerprinting. Each lot is verified for key active marker compounds (e.g., Glabridin %, Magnolol %, Eleutheroside B+E %) to match strict client target specifications prior to Certificate of Analysis (COA) sign-off.
Every shipment is backed by a full regulatory packet including COA, Technical Data Sheet (TDS), Safety Data Sheet (MSDS), Heavy Metal & Pesticide Residue Screening Reports (Eurofins/SGS certified), Non-GMO Statement, Allergen Declaration, and BSE/TSE-Free Certificates.
Yes. We specialize in OEM/ODM customization including liquid sublingual drops, custom mesh powder sizing, oil solubilization, micro-encapsulation, and private label packaging (customized amber jars, bottles, or bulk 25kg fiber drums) tailored to your brand’s retail requirements.
For standard active powders and cold-pressed extracts in stock, the Minimum Order Quantity starts as low as 1 kg. Custom OEM orders typically require an MOQ of 10-50 kg. Production lead times range from 7 to 12 working days, with express air freight and ocean shipping options direct from Shenzhen port hubs.
Explore our full line of tested botanical concentrates ready for international dispatch.




 Bluidge Biology


